 Xem Studiomeasured geometry
Library › Stirling engines › Tri-clamp engine parts ·
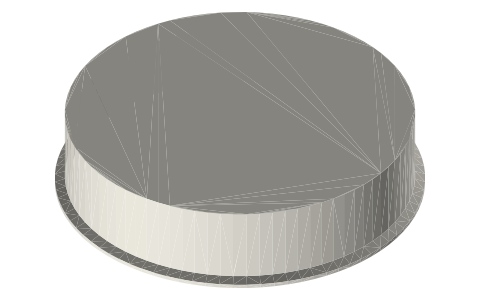
HTD hot cup: 10 in tri-clamp closed-end cup (welded floor)
How do I make a 10 inch tri-clamp hot end with no gasket in the flame? · Hardware · basis: Fabrication spec: an L14AM7-type 10 in ferrule end on Ø254 × 3.40 tube, closed by a 12.7 plate welded flush with the tube OD; exact geometry
Long Earth Society build part. Parts of the HTD engines. The engines
Exact dimensions. Every file is drawn at true size with no printing tolerance. The holes and pins that meet another part are listed below under Mating features, with the fit each joint needs; open those by your printer's or process's clearance before making the part. Mating features
- sizes
- 1 in table
Notes
- The hot face is one piece: the floor is welded to the tube, so the only joint is the clamp at the top, 48 mm of tube wall above the flame (main HTD). That wall is also the engine's biggest heat leak: about 335 W conducted from a 450 °C floor to a 77 °C cap at 16 W/m·K (a lower-conductivity wall leaks proportionally less).
- Floor: 12.7 thick. At the 6 bar gauge relief setting, treated as simply supported at the bore (conservative for a welded edge), it sees 70 MPa at the centre and bows 0.25 mm (Roark Table 11.2). The floor must be rated for that at its working temperature; I hold the hot face at or below 450 °C.
- The cup's own ferrule face takes the standard 10 in gasket and clamp.
Sizes
| part | length_mm | floor_mm | chamber_face_to_floor_mm |
|---|---|---|---|
| hot-cup-10in-60.4 | 60.4 | 12.7 | 47.7 |
Mating features
Drawn at the exact size. Open press, slide, run and socket features by your process's clearance; leave designed gaps and clamp fits as drawn.
| feature | exact | mates with | fit | files |
|---|---|---|---|---|
| face | ISO 2852 10 in | gasket-10in + 10 in clamp | clamp | all |
| bore | Ø247.19 to the floor | displacer Ø240 (3.6 radial, no contact) | designed | all |
| floor weld | Ø254 × 12.7 flush with the tube OD | tube end (welded, sealed) | designed | all |
Where the files are
Other publishers' files are linked, not hosted. "verify" = check the license at the link before commercial use.
| Steel & O'Brien | Sanitary products catalog 2024: 16AMP end caps 10 / 12 in (A 0.480, B 10.570 / 12.570 in); L14AM7 ferrules 1.500 in; clamp ratings 13MHHM, 13MHP, 13ASME | publisher's catalogue; dimensions cited, nothing copied | |
| Holland Applied Technologies | Sanitary tri-clamp fittings: EG14AM7 ferrules 8 / 10 / 12 in (1.500, bore 9.732 / 11.732 in, tube 10.000 / 12.000 in); EG16A caps (10.570 / 12.570 in) | publisher's catalogue; dimensions cited, nothing copied | |
| McGraw-Hill | Young & Budynas, Roark's Formulas for Stress and Strain, 7th ed.: Table 8.1 (fixed–guided beam), Table 11.2 (circular plates under uniform pressure) | book | formulas are facts verify |
| Long Earth Society | Engine builds | web, video | LES site |
Free files
★ Free files 1 parts. Generated by Xem Studio from the standard; threads are plain cylinders at major diameter. CC BY 4.0. index.json
| hot-cup-10in-60.4 | 10 in × 60.4 closed-end cup: ISO 2852 face, Ø254 × 3.40 tube, 12.7 floor welded flush (main HTD: chamber 51.0 face to floor with the cap) | STEP · STL |
Plain text: sheet.txt · JSON: /api/geometry?object=htd-hot-cup-10in
How it fits
In these build lists
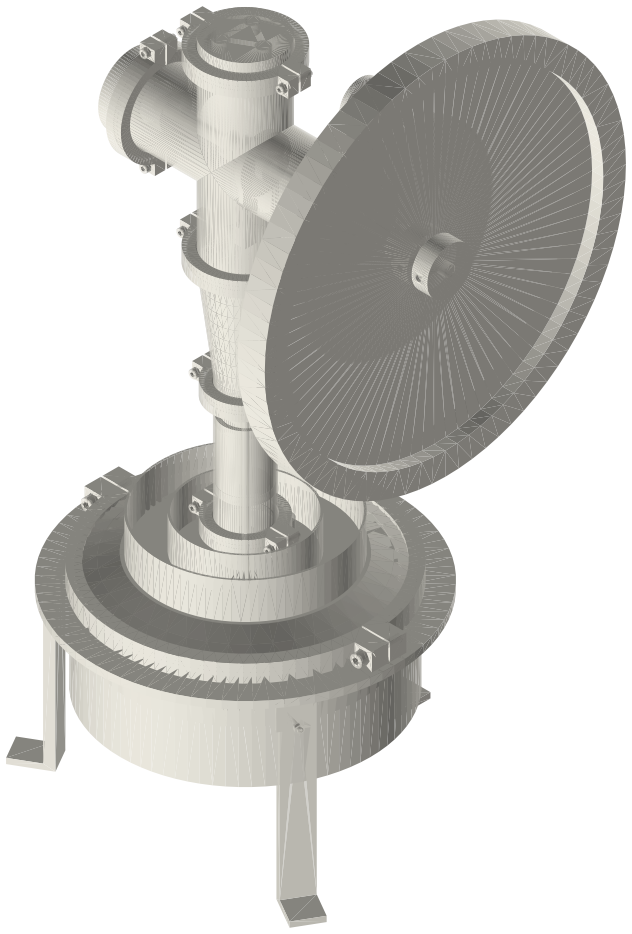
HTD engine, 10 in tri-clamp…A big flat gamma Stirling for a propane burner: a Ø240 displacer in a 10 in weld…You might also need
Questions
Why a welded floor instead of a cap?
A cap would put a gasket and a clamp in the flame. With the floor welded on, the only joint sits up at the cold cap.