 Xem Studiomeasured geometry
Library › Hardware › Stirling & thermoacoustic ·
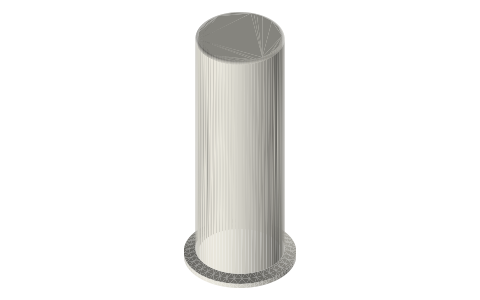
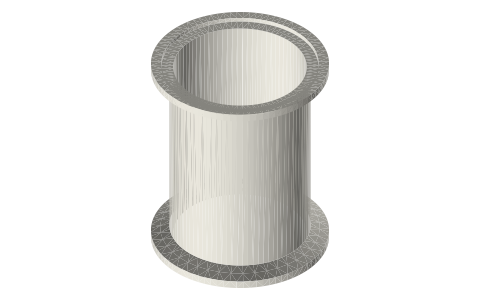
2 in × 152.4 mm closed-end hot spool, bore finished Ø48.00
How do I spec a one-piece closed tri-clamp hot end for a pressurised Stirling engine? · Hardware · basis: ISO 2852 face and ASME BPE 2 in tube as the ferrule and spools on this site; the closed end and the finished bore are design values
Long Earth Society build part. My one-piece hot end for the performance engines: one joint, at the cold face. The engines
Exact dimensions. Every file is drawn at true size with no printing tolerance. The holes and pins that meet another part are listed below under Mating features, with the fit each joint needs; open those by your printer's or process's clearance before making the part. Mating features
- sizes
- 4 in table
Notes
- A fabrication spec: a standard 2 in ferrule end, 16 ga tube and a 3 mm closed end welded into one piece, 152.4 mm (6 in) from the face to the outer end, 1.5 mm outer round on the end. Plain outside: the fin sleeve and the water jacket are separate parts that slide or clamp on. Nothing that seals is near the flame; the only joint is the clamp face.
- After the end is closed, the bore is finished Ø48.00 from the face to the floor (149.4 deep). That size cleans up any 2 in tube within its OD and wall tolerances, and the slotted liner's fin tips are a press fit in it.
- Inside, from the face: the liner's cold ring and ports, the cooler zone (z 9–54, under the water jacket), the regenerator (54–94), the heater zone (94–144, under the fin sleeve) and the hot space at the floor.
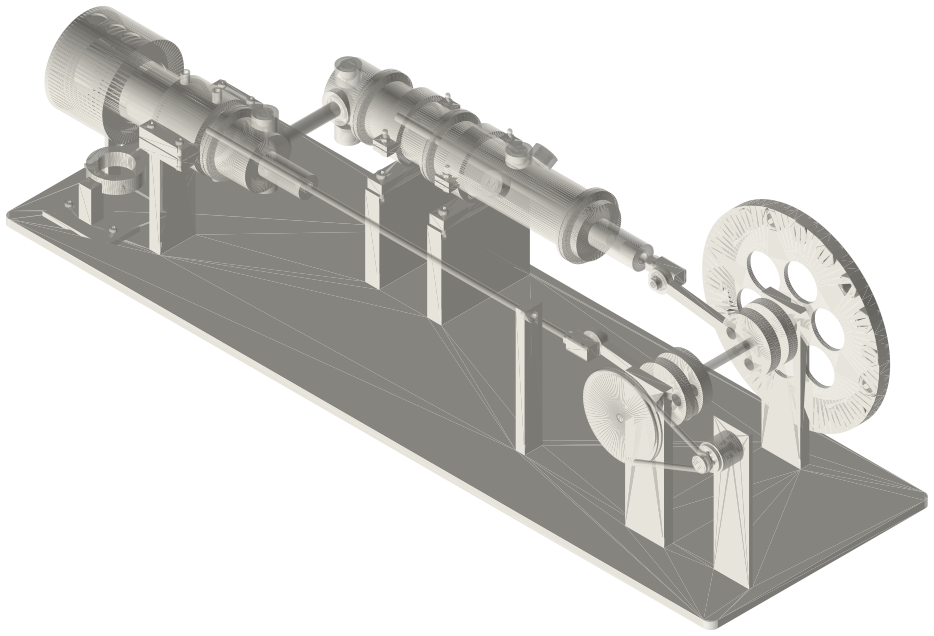
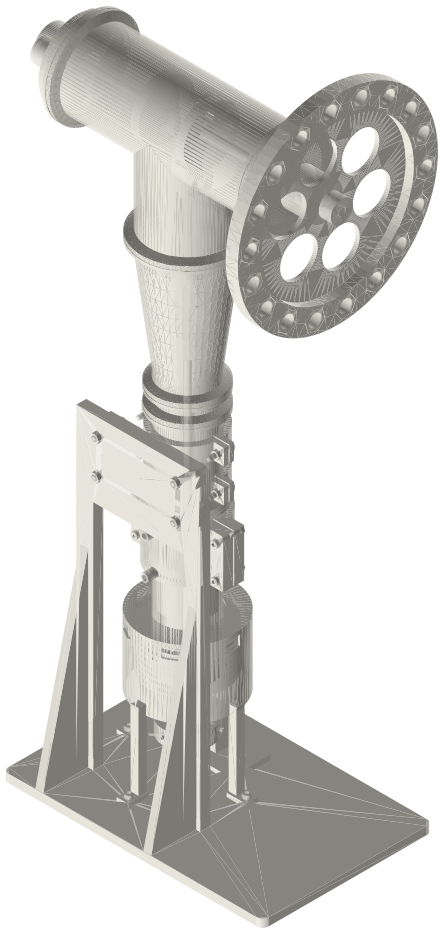
- I use it on both performance engines: lying down in the horizontal gamma and standing in the charged beta.
Sizes
| feature | value |
|---|---|
| face | ISO 2852 2 in |
| face to outer end | 152.39999999999998 |
| closed end | 3, 1.5 outer round |
| finished bore | Ø48.00 × 149.4 |
Mating features
Drawn at the exact size. Open press, slide, run and socket features by your process's clearance; leave designed gaps and clamp fits as drawn.
| feature | exact | mates with | fit | files |
|---|---|---|---|---|
| face | ISO 2852 2 in (land Ø56.5–Ø64, rim 2.85, 1.6 recess, 20° back) | Type B gasket, 2 in clamp | clamp | all |
| finished bore | Ø48.00 × 149.4 (face to floor) | liner cold ring Ø48.00 (slide) and fin tips Ø48.00 (press) | press | all |
| tube OD | Ø50.8 | fin sleeve bore, water-jacket halves, cradle seat | slide | all |
| closed end | flat outer face, 1.5 round | fin sleeve inside bottom | slide | all |
Where the files are
Other publishers' files are linked, not hosted. "verify" = check the license at the link before commercial use.
| ISO (via iTeh sample) | ISO 2852 clamp liners: face profile and flange / groove diameters | standard excerpt; dimensions are facts | |
| ASME | BPE Bioprocessing Equipment (clamp fitting dimensions, tube OD and wall) | standard | ASME; dimensions are facts verify |
| Long Earth Society | Engine builds | web, video | LES site |
Free files
★ Free files 1 parts. Generated by Xem Studio from the standard; threads are plain cylinders at major diameter. CC BY 4.0. index.json
| hot-spool-2in-152.4-closed-bored-48.00 | 2 in × 152.4 closed-end hot spool, one piece: ISO 2852 face, Ø50.8 × 1.65 tube, 3.0 closed end with a 1.5 outer round; bore finished Ø48.00 × 149.4 (to the floor) | STEP · STL |
Plain text: sheet.txt · JSON: /api/geometry?object=tri-clamp-closed-hot-spool-bored
How it fits
In these build lists
Tri-clamp horizontal gamma generator, 2 in,…The classic desk Stirling generator in tri-clamp, built for power: a horizontal …Tri-clamp walking-beam gamma generator, 2 in,…The classic desk walking-beam Stirling in tri-clamp: a standard 2 in tee with th…Tri-clamp charged beta, 2 inA standing beta that holds a charge: the same hot spool, liner, regenerator and …Tri-clamp twin walking-beam gamma generator, 2…Two walking-beam tee units side by side on one crank, a quarter turn apart: each…You might also need
Questions
Why a closed end instead of a cap?
A gasket in the flame is the first thing to fail on a charged engine. A closed end puts the only joint at the cold face.
Why bore it?
Stock 2 in tube is made to its OD and wall, not its bore. Finishing the bore to Ø48.00 makes it round and on size for the liner's press fit.